
ER308L Supplier / 304 & 304L Filler Metals
ER308L is a low-carbon austenitic stainless steel welding wire designed primarily for welding 304 and 304L stainless steels. It is widely used for MIG and TIG welding where good weldability, corrosion resistance, and resistance to intergranular corrosion are required.
With a maximum carbon content of 0.03%, ER308L reduces the risk of carbide precipitation and sensitization in the weld metal. It is therefore a preferred filler metal for general fabrication of 18Cr-8Ni stainless steels, including equipment, tanks, piping, food processing machinery, and chemical processing components.
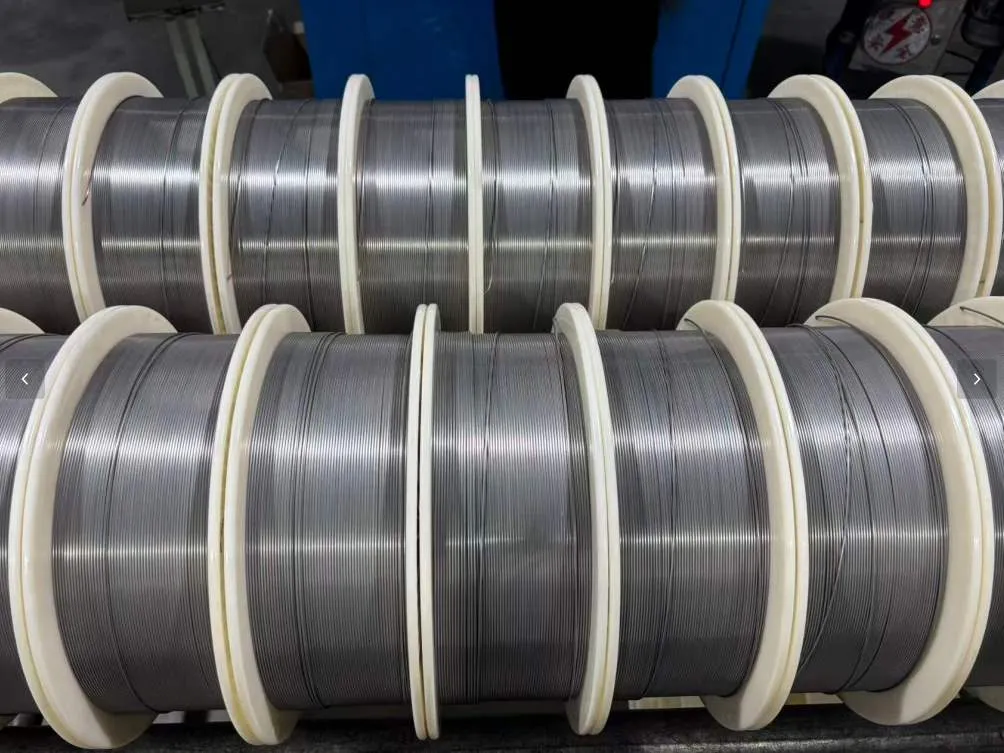
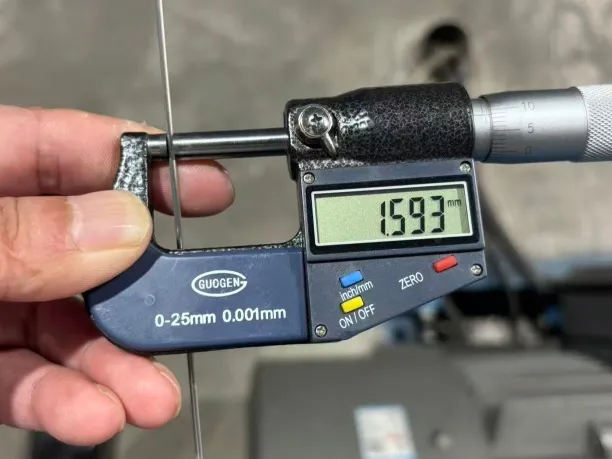
Our ER308L is available as MIG welding wire and TIG filler rod in various diameters and packaging options for industrial and fabrication applications.
📧 Email us for a quotation: support@ronsteel.com

ER308L
ER308L
ER308L
| Standard | Classification |
|---|---|
| AWS A5.9 / ASME SFA 5.9 | ER308L |
| EN ISO 14343-A | G 19 9 L |
| EN ISO 14343-B | SS308L |
| UNS | S30880 / S30883* |
* UNS designation may vary according to the applicable specification or product form. Please contact us for confirmation against your required standard or material certificate.
ER308L is primarily used for GMAW (MIG) and GTAW (TIG) processes. The corresponding covered electrode for manual SMAW welding is generally E308L-16, classified under AWS A5.4.
| C | Mn | Si | Cr | Ni | P | S | Mo | Cu | Fe |
|---|---|---|---|---|---|---|---|---|---|
| ≤0.03 | 1.0–2.5 | ≤0.65 | 19.0–22.0 | 9.0–11.0 | ≤0.03 | ≤0.03 | ≤0.75 | ≤0.75 | Balance |
Low carbon content improves resistance to intergranular corrosion in welded structures.
| Property | Typical / Specification Value |
| Tensile Strength | ≥520 MPa |
| Yield Strength | Typically ≥350 MPa |
| Elongation | Typically ≥30% |
Ø Low Carbon Content: The carbon content is limited to a maximum of 0.03%, reducing carbide precipitation and helping minimize the risk of intergranular corrosion after welding.
Ø Excellent Weldability: ER308L provides stable arc performance, good weld pool control, and smooth metal transfer, making it suitable for both production welding and general stainless steel fabrication.
Ø Good Corrosion Resistance: The chromium-nickel composition provides good general corrosion resistance for a wide range of atmospheric, food-processing, chemical, and industrial environments.
Ø Suitable for 304 and 304L Stainless Steel: ER308L is the commonly selected filler metal for joining 304/304L stainless steels and other similar 18Cr-8Ni austenitic stainless steels. It can also be used for selected stabilized grades such as 321 and 347 when service conditions are appropriate.
Ø Good Resistance to Weld Cracking: The balanced Cr-Ni composition produces a controlled amount of ferrite in the weld metal, helping improve resistance to hot cracking during welding.
| Welding Process | Typical Shielding Gas | Polarity |
| MIG / GMAW | Argon-based gas mixtures | DCEP |
| TIG / GTAW | 100% Argon | DCEN |
For GMAW, argon-based shielding gases with small additions of CO₂ or O₂ are commonly used depending on the welding procedure and required transfer mode. TIG welding generally uses 100% argon shielding gas.
Actual voltage, current, wire feed speed, shielding gas flow rate, and welding technique should be selected according to wire diameter, base-metal thickness, joint configuration, and applicable WPS.
ER308L is primarily recommended for welding:
For applications involving high-temperature service, severe corrosion, or dissimilar stainless steel combinations, filler-metal selection should be confirmed according to the base-metal grades and service conditions.
ER308L stainless steel welding wire is widely used in:
ER308L is particularly suitable for applications where 304/304L stainless steel, good weldability, and general corrosion resistance are the primary requirements.
We can supply ER308L in different forms and specifications according to welding process and application:
| Product Form | Process | Typical Sizes |
| MIG Welding Wire | GMAW | 0.8, 1.0, 1.2, 1.6 mm and other sizes |
| TIG Filler Rod | GTAW | 1.6, 2.0, 2.4, 3.2, 4.0 mm and other sizes |
Available spool, coil, tube, and carton packaging can be customized according to diameter, order quantity, and customer requirements.
The main difference is carbon content.
ER308L has a maximum carbon content of 0.03%, while standard ER308 permits a higher carbon content. The lower carbon level of ER308L reduces the risk of carbide precipitation and intergranular corrosion after welding.
For welding 304L and applications where resistance to weld sensitization is important, ER308L is generally the preferred choice.
Looking for a reliable ER308L welding wire supplier for your next project?
Send us your requirements for diameter, quantity, welding process, and destination. Our sales and technical team will confirm the suitable specification, packaging, lead time, and provide a competitive quotation.
📧 Email: support@ronsteel.com


 English
 Español
 русский язык
 اللغة العربية