
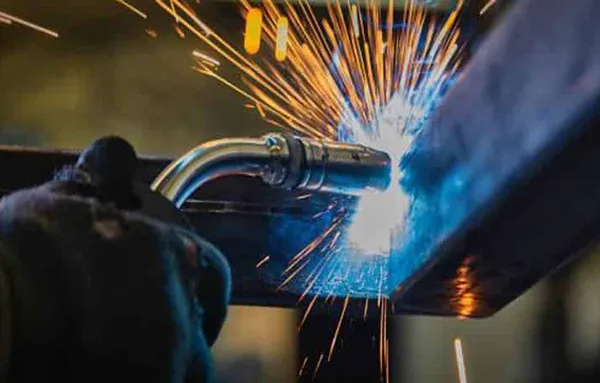
For most thick carbon and structural steel applications, E7018 is the best all-around welding rod because of its low-hydrogen characteristics, good strength, ductility, and suitability for multi-pass welding.
However, the best rod depends on the job:
There is no universal thickness that officially defines "thick metal". In practice, thicker sections become more demanding when they require joint preparation, multiple passes, preheating, or greater control of heat input and hydrogen.
| Metal Thickness | Typical Consideration |
|---|---|
| Under 1/4" (6 mm) | Light to medium fabrication |
| 1/4"–1/2" (6–12 mm) | Electrode size and heat control become more important |
| 1/2"–3/4" (12–19 mm) | Joint preparation and multiple passes are commonly required |
| Over 3/4" (19 mm) | Preheat, interpass temperature, and hydrogen control become more important |
The actual electrode selection should be based on the base metal, joint design, welding procedure, and applicable code, rather than thickness alone.
Before diving into specific recommendations, you need to decode the numbers stamped on every welding rod. The AWS A5.1 classification system tells you important information about the electrode:
For thick metal, coating type matters because restrained joints and cooling conditions can increase cracking concerns. Low-hydrogen electrodes such as E7018 are commonly selected when hydrogen control is important.
Cellulosic electrodes such as E6010 provide deep penetration and are particularly useful for root passes, but they are not a direct substitute for a low-hydrogen electrode in every thick-section application.
| Electrode | Tensile Strength | Penetration | Best Use on Thick Metal | Position | Polarity |
|---|---|---|---|---|---|
| E7018 | 70,000 psi | Moderate | Structural fill/cap, code work | All | DCEP or AC |
| E6010 | 60,000 psi | Very Deep | Root passes, dirty steel | All | DCEP only |
| E6011 | 60,000 psi | Deep | Root passes, AC machines | All | AC or DCEP |
| E8018 | 80,000 psi | Moderate | High-strength thick steel | All | DCEP or AC |
| E7014 | 70,000 psi | Shallow-Medium | High-deposition flat work | All | AC or DCEN |
Always check the manufacturer's product data and applicable welding procedure for operating characteristics.
If you're welding thick carbon steel such as structural frames, heavy equipment, or other heavy-fabrication applications, E7018 is usually the best all-around choice.
It produces 70,000 psi minimum tensile strength weld metal and provides good ductility and low-hydrogen performance. These characteristics make it particularly suitable for restrained joints and multi-pass welding.
For code-governed work, electrode selection should follow the applicable welding procedure and requirements of standards such as AWS D1.1 or ASME Section IX rather than thickness alone.
Getting the amps right is critical. Under-amping can contribute to incomplete fusion and slag inclusions, while excessive current can make the weld difficult to control.
| Rod Diameter | Amperage Range (DCEP) | Typical Use |
|---|---|---|
| 1/8" (3.2 mm) | 110–150 A | Smaller/heavier fabrication passes |
| 5/32" (4.0 mm) | 140–190 A | 1/2" to 3/4" plate applications |
| 3/16" (4.8 mm) | 180–250 A | 3/4" and thicker applications |
Actual amperage should be selected according to electrode specifications, welding position, joint design, and the applicable welding procedure.
E7018 is a low-hydrogen electrode and must be protected from moisture. Once the package is opened, follow the manufacturer's storage, holding, and rebaking requirements to maintain the intended low-hydrogen characteristics.
E6010 and E6011 are cellulosic electrodes that produce an aggressive, digging arc with deep penetration.
E6010 is commonly used for open-root pipe welding because its fast-freeze puddle provides good root control. It runs on DCEP.
E6011 provides similar deep-penetrating characteristics while also working with AC, making it useful with AC welding machines.
Cellulosic electrodes are not automatically the best choice for the entire weld on thick, restrained, or crack-sensitive joints. Where the welding procedure requires low-hydrogen electrodes, E7018 or another approved low-hydrogen electrode may be required for subsequent passes.
For E6010 and E6011, amperage depends on electrode diameter, welding position, joint design, and the manufacturer's recommended range. Always follow the electrode manufacturer's specifications rather than using thickness alone to determine current.
E8018 delivers 80,000 psi minimum tensile strength and is selected when the base metal or welding procedure requires higher-strength weld metal.
It can be appropriate for high-strength low-alloy steels and applications where matching weld-metal strength is necessary.
Higher strength does not automatically mean better performance. For standard structural carbon steel, E7018 may be the more appropriate choice when its strength and toughness characteristics meet the welding requirements.
Rod diameter should be selected based on metal thickness as well as joint design, welding position, available amperage, and pass sequence.
| Metal Thickness | Typical Rod Diameter | Typical Application |
|---|---|---|
| Under 4 mm | 2.0–3.2 mm | Thin sheet, tack welds |
| 4–12 mm | 3.2–4.0 mm | General fabrication |
| Over 12 mm (1/2") | 4.0–5.0 mm | Thick plate, structural work |
| Over 3/4" | 4.8 mm and larger where appropriate | Heavy structural work |
A 3/16" (4.8 mm) electrode can be useful for heavy fabrication, but electrode diameter should not be selected from plate thickness alone. Welding position, joint design, equipment, and the required pass sequence also matter.
For 1/2" steel, for example, 1/8" or 5/32" E7018 electrodes may be used depending on the joint and welding procedure.
Rod selection is only part of the equation. Thick metal welding may require several process adjustments.
Joint preparation: Bevel thicker sections when required to provide proper root access and sidewall fusion.
Preheat: Preheat requirements depend on steel grade, thickness, restraint, hydrogen level, and the applicable welding procedure. Do not apply one fixed preheat temperature to every thick-steel application.
Multi-pass strategy: Thick plate is commonly welded using multiple passes rather than a single oversized electrode. A root pass may use E6010/E6011 where appropriate, followed by E7018 or another procedure-approved electrode for fill and cap passes.
Travel and electrode angle: Maintain the angle and travel speed recommended for the electrode, welding position, and joint type to achieve proper fusion and bead shape.
| Application | Best Rod | Why |
|---|---|---|
| Structural steel (AWS D1.1) | E7018 | Low-hydrogen characteristics and good toughness |
| Pipe root passes | E6010 | Deep penetration and fast-freeze puddle |
| Heavy equipment repair | E7018 | Good ductility and low-hydrogen performance |
| High-strength steel | E8018 | Higher-strength weld metal when required |
| Dirty/rusty thick steel | E6011 | Deep penetration and better tolerance for contaminants |
| High-deposition flat work | E7014 | Higher deposition rate |
For most carbon and structural steel applications, E7018 is the best all-around choice for 1/2-inch steel. A 1/8" or 5/32" electrode may be selected depending on joint design, welding position, and pass sequence.
For 1-inch carbon or structural steel, E7018 is commonly used when it meets the base-metal and welding-procedure requirements. Thick sections may require proper joint preparation, preheat, and multiple passes.
E6010 provides very deep penetration among the common electrodes discussed here. E6011 also provides deep penetration and can be used with AC welding machines.
They serve different purposes. E6010 is generally better for deep-penetrating root passes, while E7018 is better suited to low-hydrogen fill and cap passes in many structural applications.
It depends on the base metal and welding procedure. E6011 can be suitable for some applications, but low-hydrogen electrodes may be required for crack-sensitive or code-governed work.
There is no single best size. 1/8", 5/32", and 3/16" electrodes are commonly used for thick-steel applications, with the final choice depending on joint design, welding position, equipment, and required deposition rate.
E7018 should be stored and handled according to the manufacturer's requirements to prevent moisture pickup. Proper storage is important because moisture can increase hydrogen levels and affect weld quality.
Ronsco is a trusted global supplier of nickel alloy and stainless steel welding wires, including Inconel, Hastelloy, and Monel series. Our products are manufactured to meet industry standards and are widely used in demanding applications such as aerospace, oil & gas, chemical processing, and power generation. Explore our resource center for the latest industry insights, product knowledge, and technical references.
Contact us for a quote or technical assistance.


 English
 Español
 русский язык
 اللغة العربية